
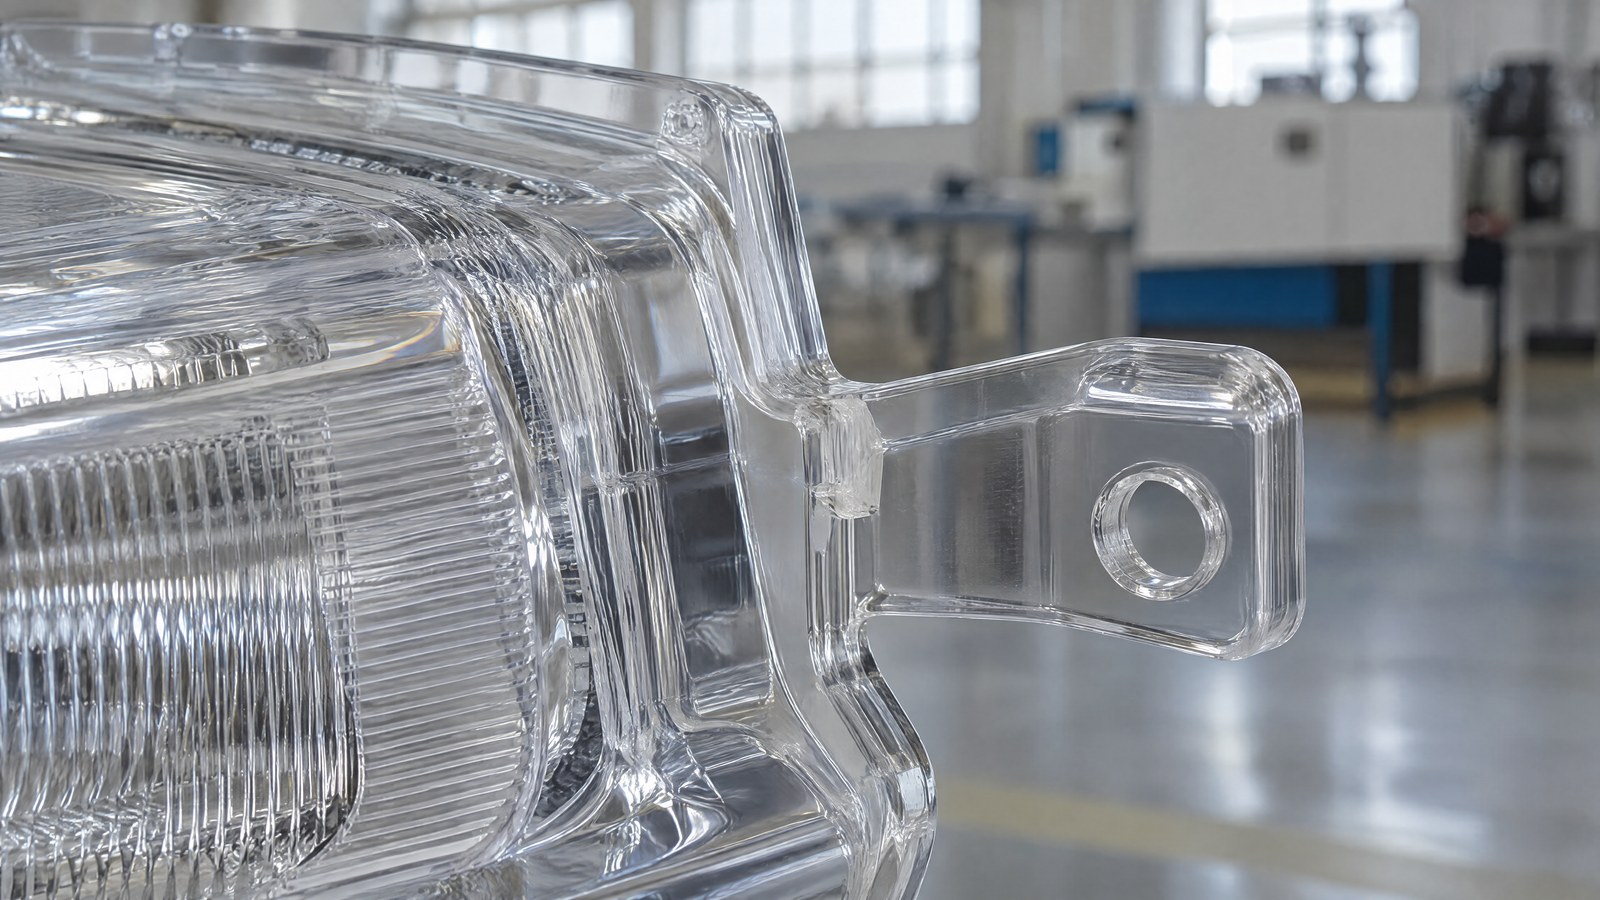
Anyone who injection-moulds plastic components knows the final step of the cycle well: separating the part from the sprue, the solidified feed channel that carries the molten resin into the cavity. It is an apparently trivial operation, yet it is here that the appearance of the break point, the cleanliness of the surface and, often, the quantity of rejects that fail visual inspection are all decided.
Separation can be done in two very different ways. Mechanical cutting — shearing, clipping, nippers — is the traditional method and remains valid on many production runs. Laser degating separates the sprue without contact, with a beam that works the material at the break point. This article compares the two approaches on what really matters to anyone managing production: edge quality, residues, wear, repeatability and in-line integration — while also saying when mechanical cutting remains the most sensible choice.
Sprue separation is a critical point of the cycle
The sprue is not a cosmetic detail. The point where it was attached (the gate) is a transition zone between the functional geometry of the part and waste material, and the way separation happens leaves a permanent mark. On a visible component — a frame, a light guide, an automotive interior panel — that point must be flat and clean; on a functional component it must be free of cracks or deformation that could weaken the area. In both cases the separation method goes directly into the part’s quality specification.
Mechanical cutting: where it works and what it leaves on the part
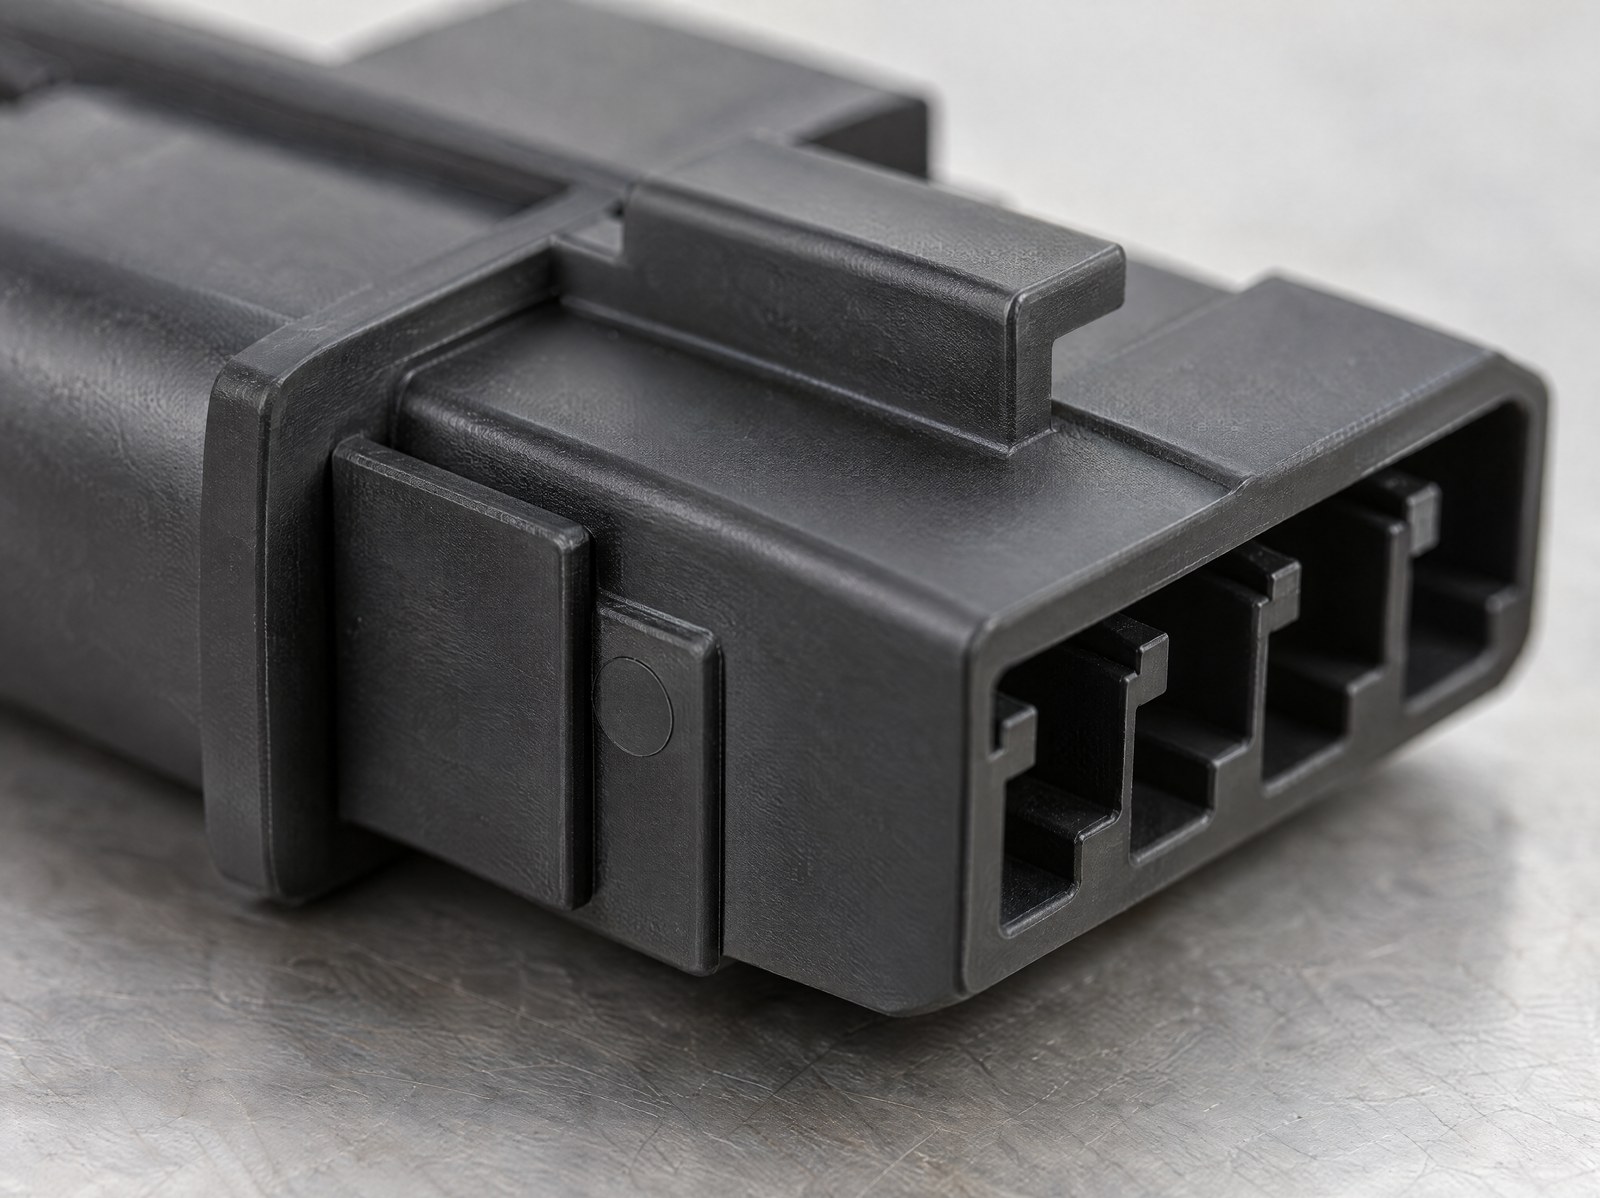
Mechanical cutting is fast, direct and perfectly adequate when the gate is thick, the geometry of the break point is accessible and the cosmetic tolerance is wide. A well-sharpened blade or nipper on a resin that cuts cleanly produces an acceptable separation in fractions of a second, and this simplicity is hard to beat on high volumes of non-visible technical parts.
The limits arise when the part is visible or the material is sensitive. Tool contact exerts a stress on the separation zone: on filled, fibre-reinforced or brittle resins, this can generate microfractures, whitening (stress whitening) or an edge that frays. Burrs and flashing are then left to be finished off, and dust and small chips are produced that settle on the part or in the working environment. Finally, blades wear out: an edge that loses its sharpness progressively worsens the finish, and the moment it needs replacing does not always coincide with a controlled quality threshold.
Laser degating: separating the sprue without contact
Laser degating tackles the same problem thermally rather than mechanically. The beam is brought onto the break point and removes material along a software-defined path, separating the sprue from the part without anything physically touching the surface. The absence of contact eliminates mechanical stress on the separation zone at the root: there is no blade pressing down, so there is no load generating whitening or microfractures on delicate resins.
The cutting path is a geometric value in the programme, not the physical position of a tool. This makes the process controllable: the break point is always the same, cycle after cycle, and the edge profile depends on the set parameters, not on the sharpness of a blade. Laser sprue removal was created precisely for the cases where mechanical cutting cannot guarantee a repeatable, clean break point.
Edge and residues: the comparison that counts on the finished part
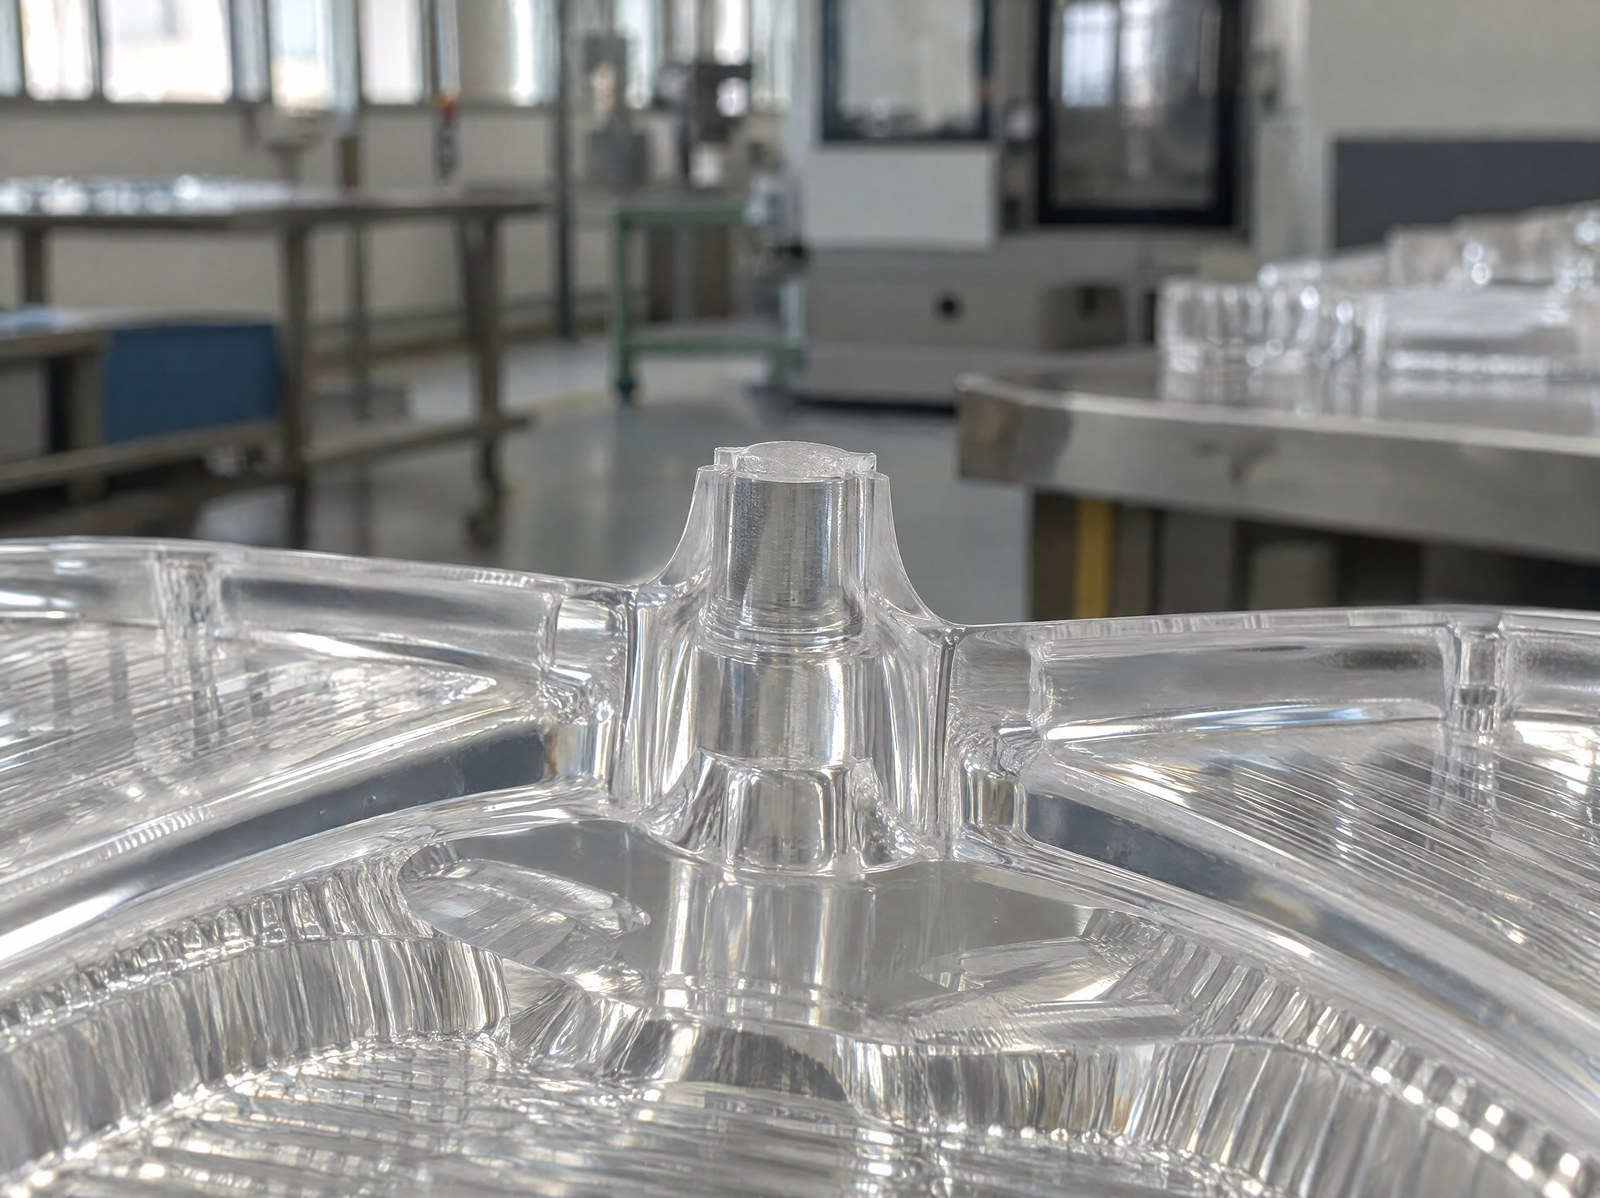
On the edge the difference can be seen by eye and felt by hand. Contactless separation tends to leave a crisp point, without the burrs and fraying typical of a blade that is losing its edge, and without the whitened zone that sometimes accompanies shearing on rigid materials. On optical lighting components this aspect has a specific and well-known implication: the residues and micro-particles left by an imprecise separation can migrate and condense on internal surfaces, a phenomenon we explored when discussing the foggy effect in laser degating. A clean edge and a process that manages fumes with localised extraction reduce the source of the problem instead of having to chase it downstream.
| Aspect | Mechanical cutting | Laser degating |
|---|---|---|
| Contact with the part | Blade or nipper in contact | No contact |
| Break-point edge | Possible burrs and fraying | Crisp edge, no burrs |
| Residues | Dust and chips on the part | Fumes managed with localised extraction |
| Stress on the separation zone | Mechanical stress present | Mechanical stress absent |
| Wear | Blades to sharpen and replace | Process with no cutting edge to replace |
| Variant changeover | New tooling or jigs | New path in the programme |
Repeatability and wear: what changes on high volumes
On a single part the two technologies can give close results; it is over the life of the run that the paths diverge. In mechanical cutting, edge quality is tied to a part that wears out: as the blade loses its edge, flashing increases and stress on the part grows, up to replacement. This introduces variability across the batch that must be controlled with inspections and scheduled maintenance.
Laser degating has no cutting edge that wears away: the result depends on stable parameters and the programmed path, so the edge of the first part and that of the last in the run are governed by the same logic. For production that measures quality in terms of repeatability — and that must justify it within process control — this stability is often the real argument, more than the peak quality achievable on a single sample.
In-line integration and flexibility on part changeover
Because laser degating is software-controlled, changing component means recalling a different path, not setting up new blades or dedicated jigs. On production with many variants or small batches, this flexibility affects set-up time more than any individual speed figure. The laser cell can also operate as an integrated node in the line, in sync with the press and material handling, and can combine separation with traceability marking on the same part at the same station. Mechanical cutting remains more straightforward to integrate when the geometry is fixed and the format hardly ever changes.
When mechanical cutting remains the right choice
Laser degating does not replace mechanical cutting in every situation. On very thick, heavy gates, on large-section sprues or on resins that cut cleanly and are not visible, shearing remains the simplest, fastest and cheapest route to set up: adding a laser source where a tool solves the problem well makes no technical sense. The laser is justified when the break point is critical for appearance or function, when the material is sensitive to mechanical stress, when residues are a downstream quality problem or when edge variability across the run is not acceptable. In practice, it is on visible components, on delicate or filled resins and on multi-variant production that contactless separation shows its value; elsewhere, the nipper still does its job perfectly well.

Public Relations Manager | LASIT
Public Relations Manager at LASIT since 2019, Claudia Neri is responsible for managing the Marketing and Communications department. She handles the company’s communication strategy, coordinating public relations, brand promotion and institutional communication activities for the Italian and international market.


