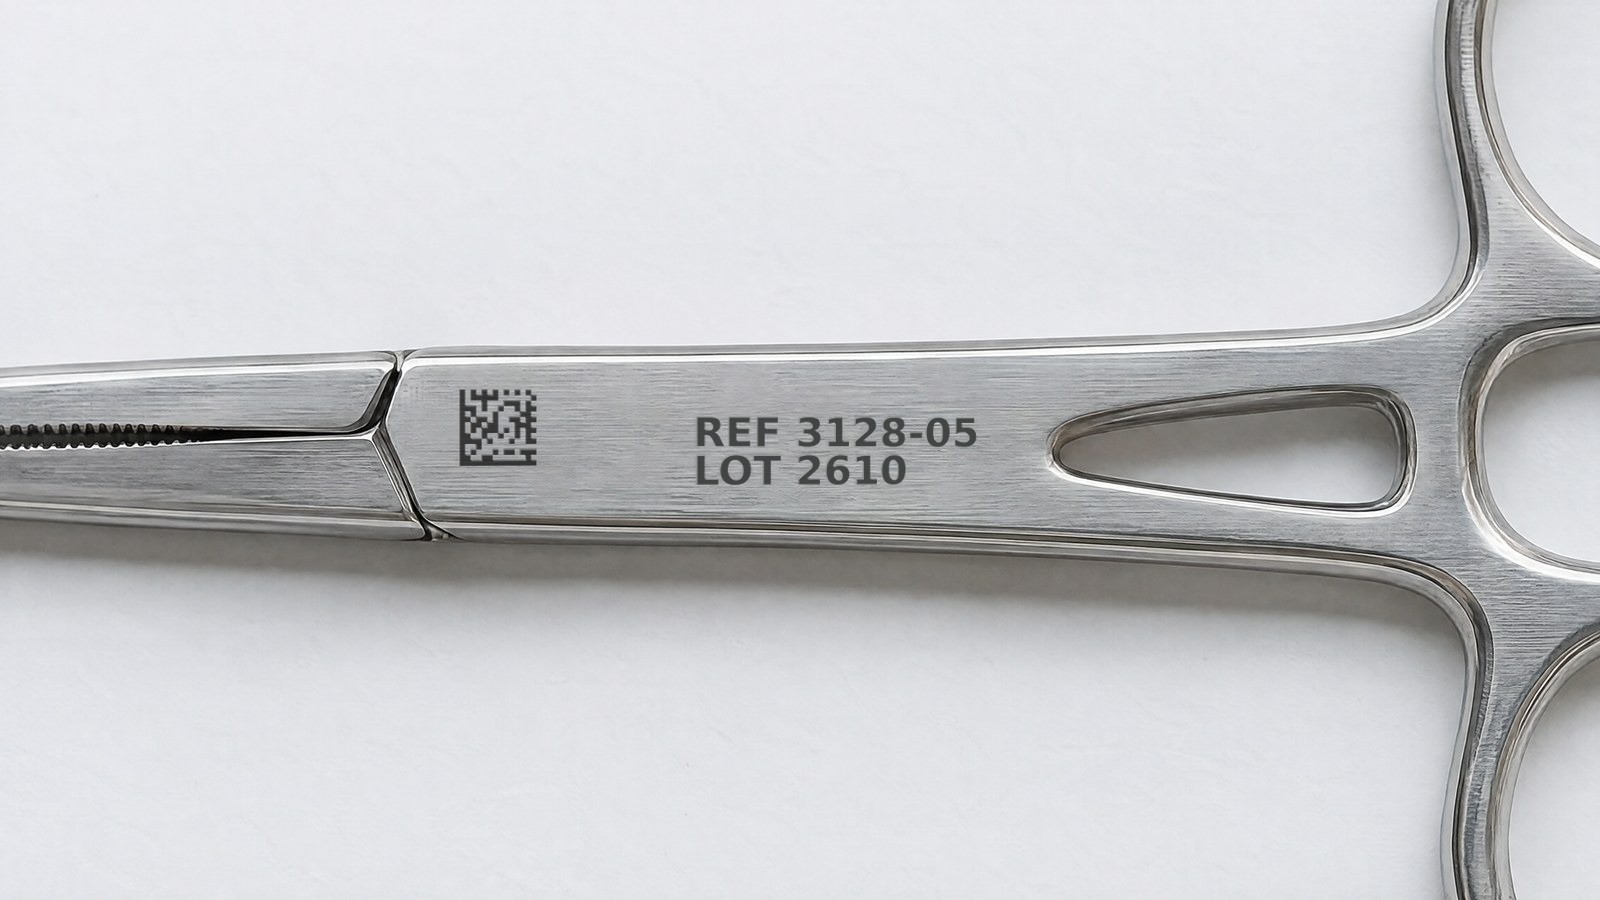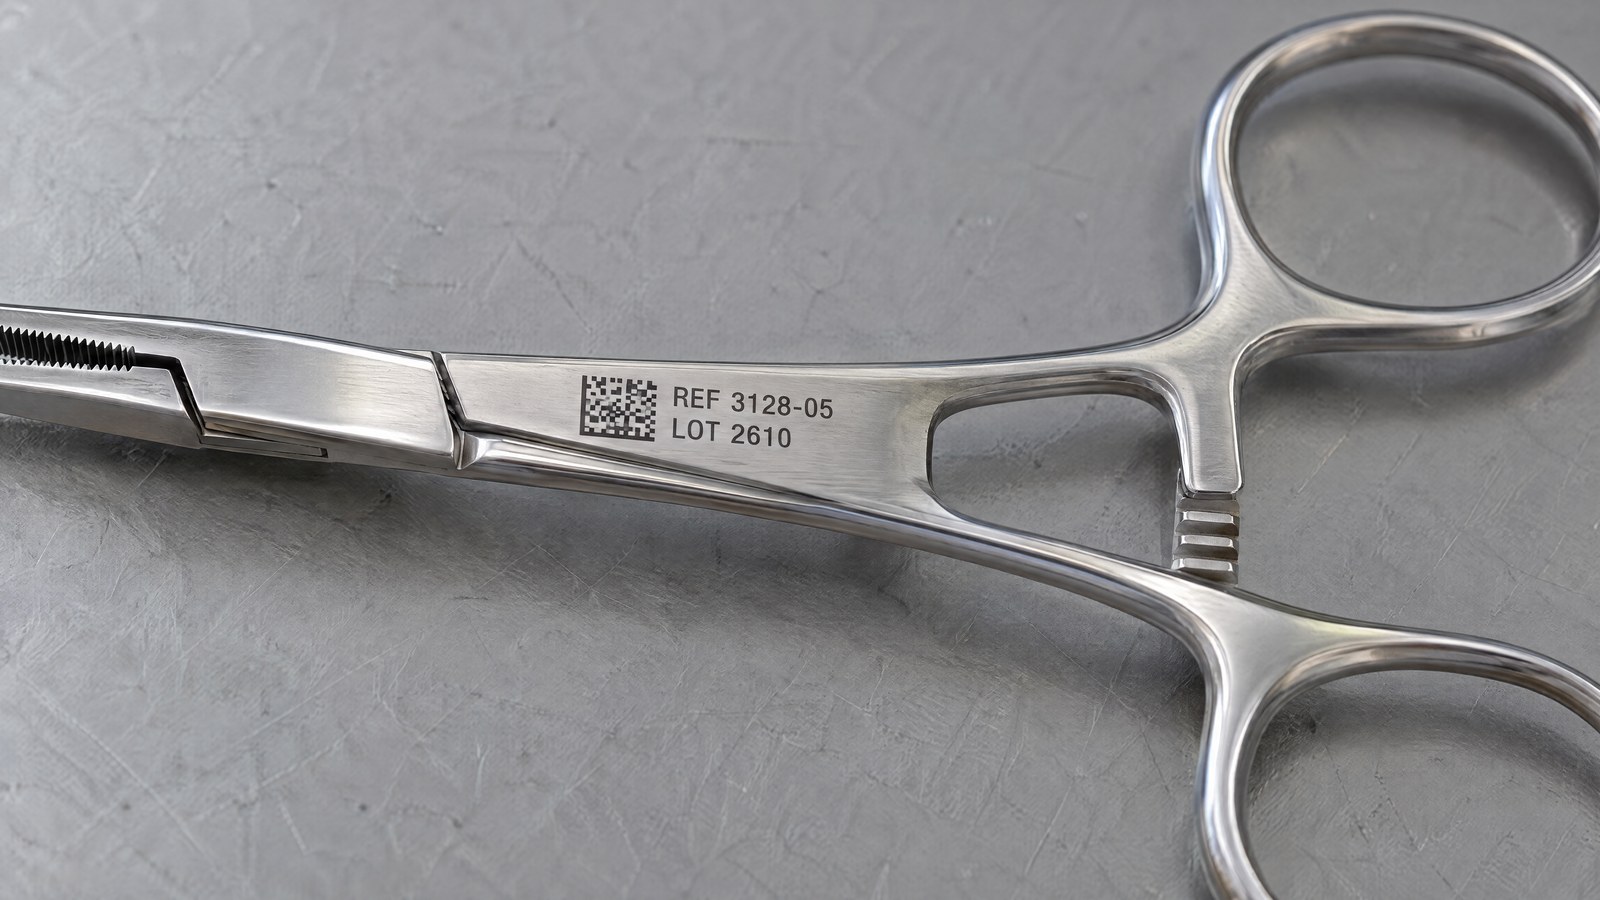
Those who manufacture reusable surgical instruments live with a constraint that permits no shortcuts: every forceps, needle holder, retractor or clamp returns to the sterilisation department dozens, often hundreds of times over its service life. With each cycle the instrument passes through washing in an alkaline solution in the washer-disinfector, rinsing and saturated steam in the autoclave. The code engraved on the handle must remain legible from the first of these cycles to the last, because instrument traceability is not a label that gets reapplied: it is a permanent piece of data bound to the item.
This is where a precise technical tension arises. To be permanent, the marking must withstand abrasion, steam and detergents; to be hygienic, the instrument’s surface cannot present cavities, grooves or micro-cracks where organic residue and biofilm can lodge and escape reprocessing. A deep marking satisfies the first requirement and jeopardises the second. It is the point at which how you mark matters as much as what you mark.
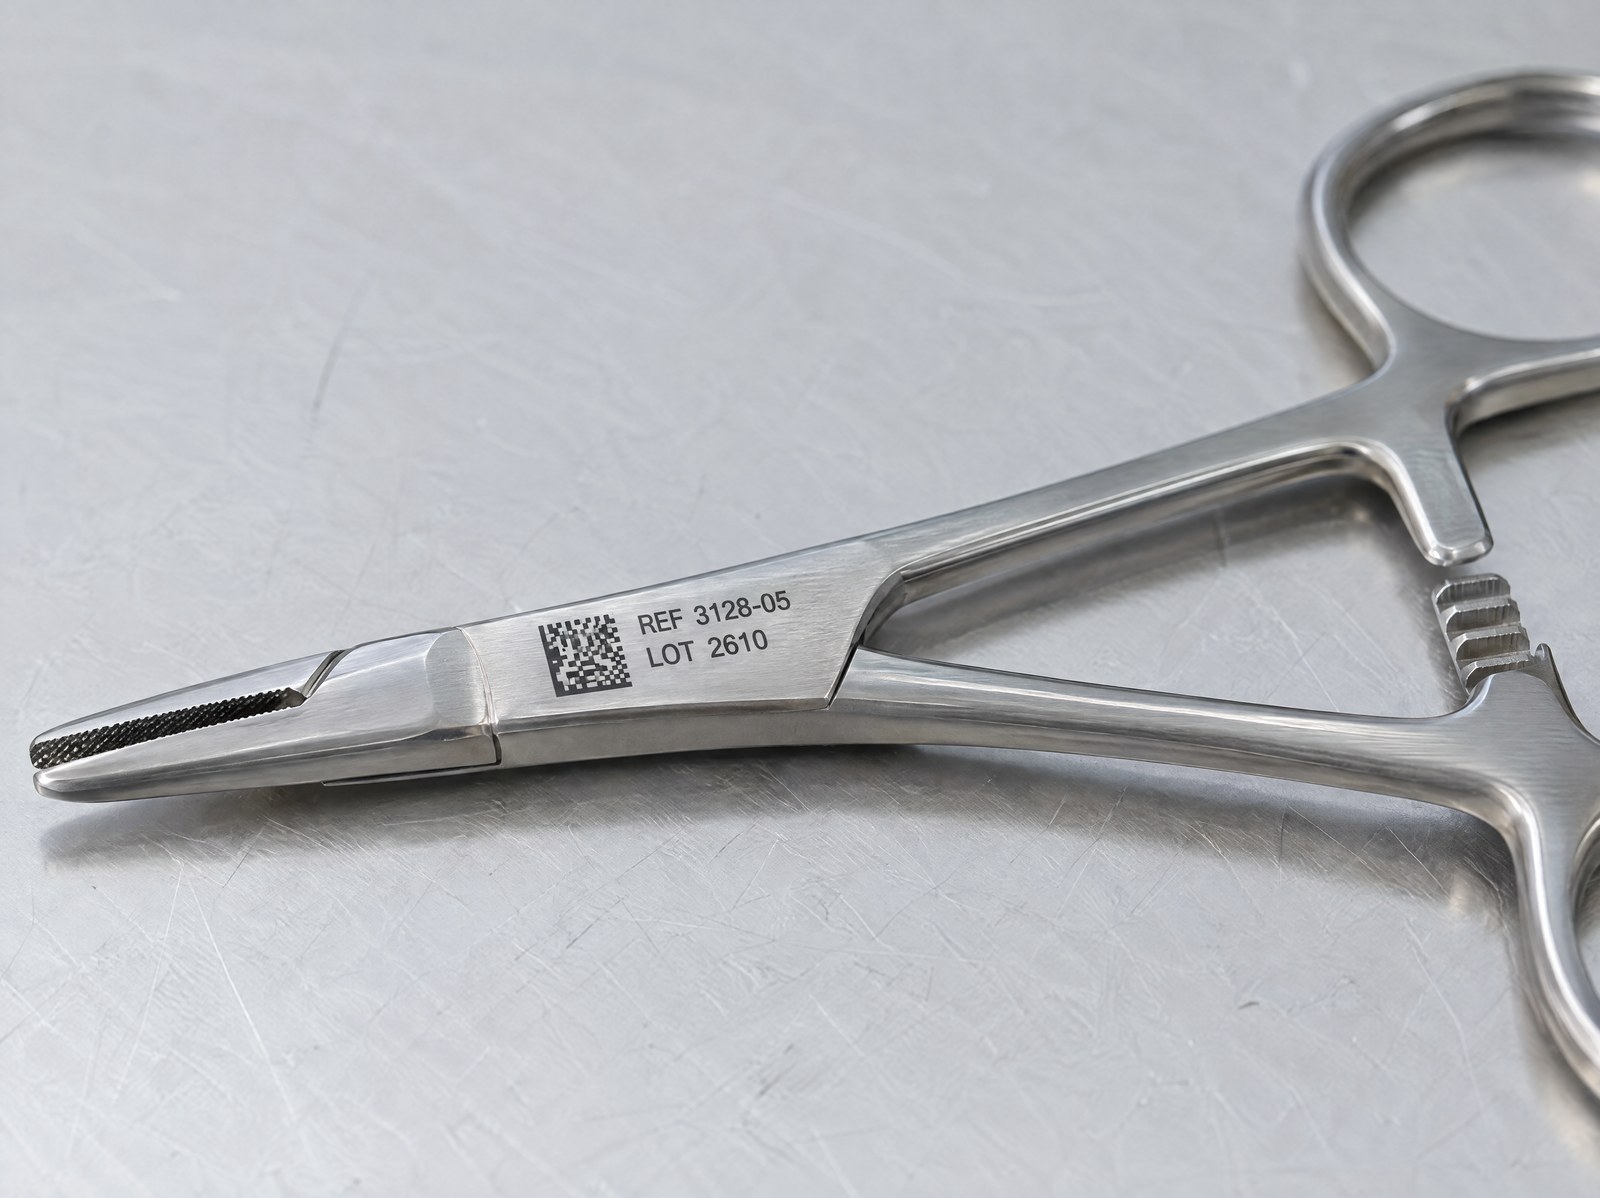
Laser annealing addresses precisely this tension: it generates a high-contrast code without removing material, because the information resides in a layer of oxide grown within the surface and not in a groove dug above it.
Why a groove is a reprocessing problem, not just an aesthetic one
On reusable instruments, the cleanability of the surface is a process requirement, not an aesthetic detail. Reprocessing must remove the organic load in a verifiable way: any geometry that retains residue — a groove, a raised edge, a micro-cavity — becomes a point where cleaning is harder to achieve and harder to demonstrate. On a device that will return to contact with the patient, a mark that digs into the surface introduces exactly this kind of retention.
Deep engraving and stamping solve permanence by creating a geometry: the mark exists because material has been removed or deformed. That same geometry, however, is a potential site of retention. The paradox is that the deeper the mark — hence the more “permanent” in a mechanical sense — the further the surface moves from the smooth, continuous condition that the sterilisation department must guarantee cycle after cycle.
Annealing: the code lies in the oxide, not in removed material
Annealing is a process of controlled oxidation. The beam of a fibre source locally heats the stainless steel below the melting and ablation threshold: the heat grows a layer of oxide beneath the surface which, through optical interference, appears dark and high in contrast. No material is removed, no crater forms. The mark is chromatic, not geometric, and the surface remains substantially continuous and coplanar with the surrounding metal.
The consequence for the medical field is direct: a DataMatrix produced by annealing introduces no new cavities on the instrument’s surface. The code is legible thanks to the contrast between the oxidised area and the polished metal, not thanks to a relief that the reader has to “feel”. The same logic of controlled oxidation governs the marking of titanium in implantable devices, where we explored controlled oxidation on titanium and UDI codes; on surgical stainless steel the principle is analogous, but calibrated to the life cycle of an instrument that is repeatedly reprocessed.
| Characteristic | Deep engraving | Annealing |
|---|---|---|
| Material removal | Yes | No |
| Groove or cavity on the surface | Present | Absent |
| Cleanability in the marked area | Reduced within the mark | Continuous surface |
| Location of the information | Excavated geometry | Oxide layer |
The quality of this layer depends on the parameters: the annealing process window must be calibrated so that the oxide is stable, uniform and free of excessive heat input, allowing the surface to retain its corrosion resistance. It is a control defined on the real material and the real geometry of the instrument, because martensitic and austenitic steels respond to heat differently.
Saturated steam and alkaline detergents: what the marking faces
The environment the code must pass through is aggressive and repetitive. In the washer-disinfector the surface meets alkaline detergents at high temperature; in the autoclave it meets saturated steam under pressure. Each cycle is a small thermochemical treatment, and a reusable instrument accumulates many of them over its service life. A poorly controlled surface marking can lighten, shift in tone or lose contrast under precisely this sequence.
The advantage of annealing is that the oxide is an integral part of the surface: it is grown from the substrate, not a deposit laid on top. A stable, cohesive oxide layer is the prerequisite for the code’s contrast to stay constant across the cycles, without the degradation typical of a mark that lives only on the very outermost skin of the surface. Verifying this behaviour, however, cannot be taken for granted: it is measured, and that is what makes the data usable in the file.
Permanent legibility of the DataMatrix: from contrast to grading
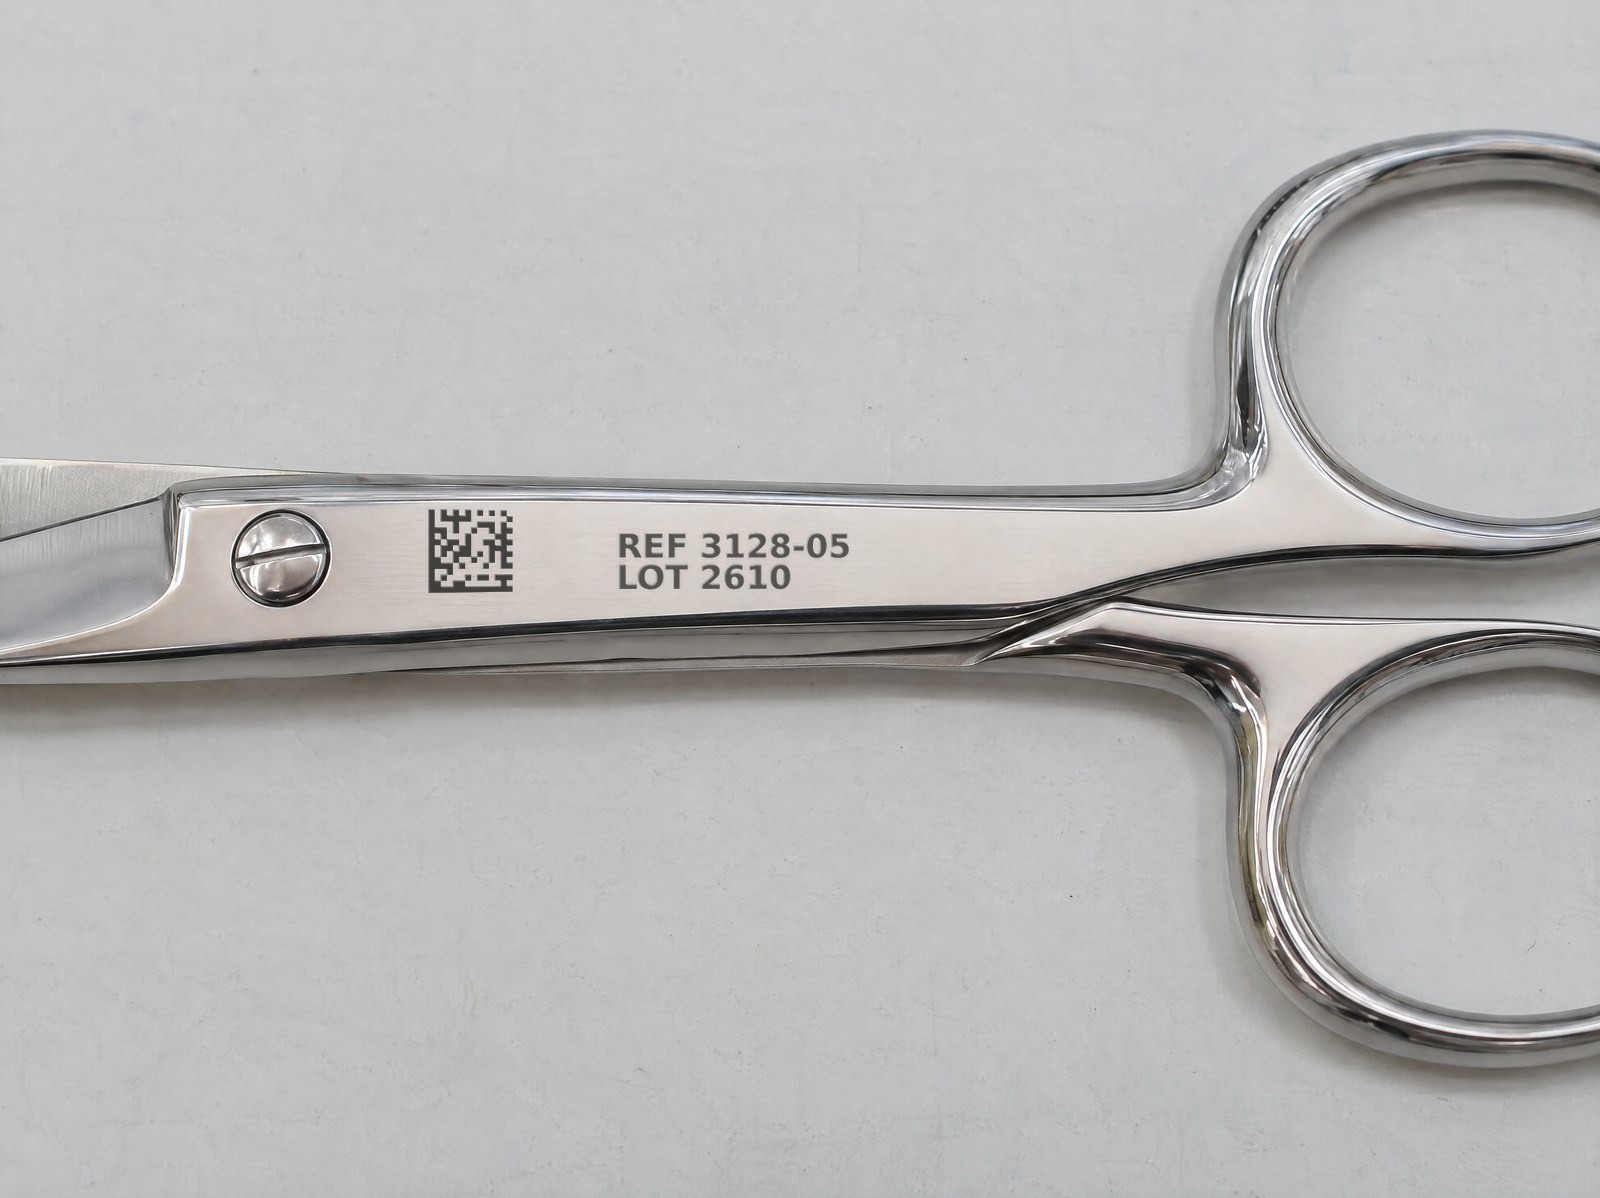
Permanent legibility means that an industrial reader decodes the code reliably throughout the instrument’s life, not just at the initial inspection. On a polished surgical surface this depends on two factors: the stable contrast between the oxidised area and the metal, and the clean geometry of the DataMatrix modules. Annealing performs well on both, because it produces a dark, matt mark that does not rely on a relief to be read.
Code quality is measured through grading, the standard applicable in line to DataMatrix codes, distinct from verification proper, which requires controlled laboratory conditions. It is an important operational distinction: these are different levels of control with different purposes, as we explained when analysing the difference between reading, grading and verifying codes. Assigning a grade to the code immediately after marking, and then returning to assess it after the reprocessing cycles, turns “legibility” from a qualitative impression into a documentable value.
Documenting the code’s durability over time for the file
A code that is permanent on paper and a code whose permanence is demonstrated are two different things. For the instrument’s technical file you need the second: a repeatable proof that the mark withstands the real sequence of reprocessing to which the device will be subjected. The path is experimental before it is documentary.
Document code durability for the fileSample markingReconditioning cyclesCode gradingRecording in the fileIn practice, representative samples of the instrument are marked, subjected to repeated cycles of alkaline washing and steam sterilisation, and at defined intervals the codes are re-read and assigned a grade. Comparing the initial grading with that after the cycles shows whether and to what extent the contrast holds, and provides the data that goes into the file. It is the same rigour with which we tackle the root of non-conformities in UDI marking on metals: conformity is not asserted, it is measured on real samples. The LASIT laboratory is designed to build this evidence on the customer’s specific materials and cycles.
Who it is designed for (and who it is not)
Annealing is the reference choice when the instrument is in stainless steel, is reprocessed many times and the surface must remain cleanable: reusable surgical instruments, forceps, needle holders, retractors, containers and components where a groove would be a hygiene problem before being a reading one. In these cases the code in the oxide combines permanence and surface continuity better than any geometric mark.
It is not, however, the universal answer. Where the requirement is a declared mechanical depth, or where the material does not develop a stable oxide useful for contrast, engraving or markings with different sources make more sense; on some high-end polished surfaces the choice of a black mark from an ultrashort pulse, whose heat input is negligible, may prevail. The rule, valid here as always, is to start from the real material and the real reprocessing cycle, not from the technology: it is the autoclave-detergent-reading sequence that tells you which marking will hold for the entire life of the instrument.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.