

In an IATF 16949-certified automotive plant, marking a component is not the last cosmetic step of the cycle: it is the moment the data that makes it traceable throughout its entire life is created. Anyone managing quality and industrialisation knows that, during an audit, it is not enough to show a well-marked part. You have to prove that the part has been marked, that the code is the one intended, that it has been read and confirmed, and that no other component carries the same identifier.
This is a substantial difference. A crisp DataMatrix on steel is a necessary condition, not a sufficient one. What holds up — or fails to hold up — under an audit is the data chain: the controlled sequence that runs from generating the code to confirming it, with a verifiable trace of every step. When this chain has a weak link, the defect does not show on the part, it shows in the records, and that is where points are lost.
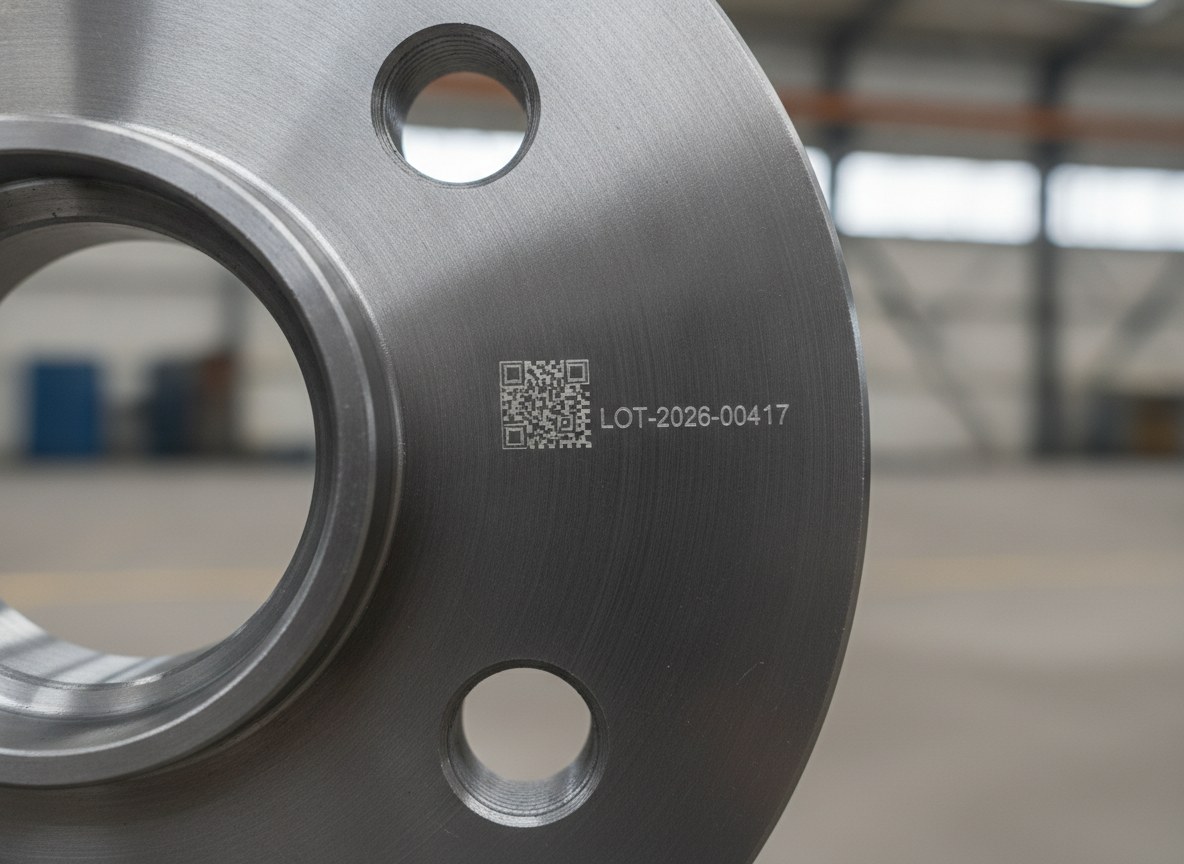
This article describes how a fibre laser marking system builds and protects that chain directly in line, from reserving the sequence number through to managing the rejected part, and which recurring errors weaken it.
Why fibre is the standard on automotive metals
The 1064 nm fibre source is the benchmark for automotive metals for a reason that matters more than speed in an audit: permanence. On steel, aluminium, cast iron and treated alloys, fibre marking survives washing, oils, handling, heat treatments and long life cycles, remaining legible for years. Traceability that relies on labels or on inkjet fails precisely where it is needed most: after an aggressive process or at the end of the component’s life, when the code has to be re-read.
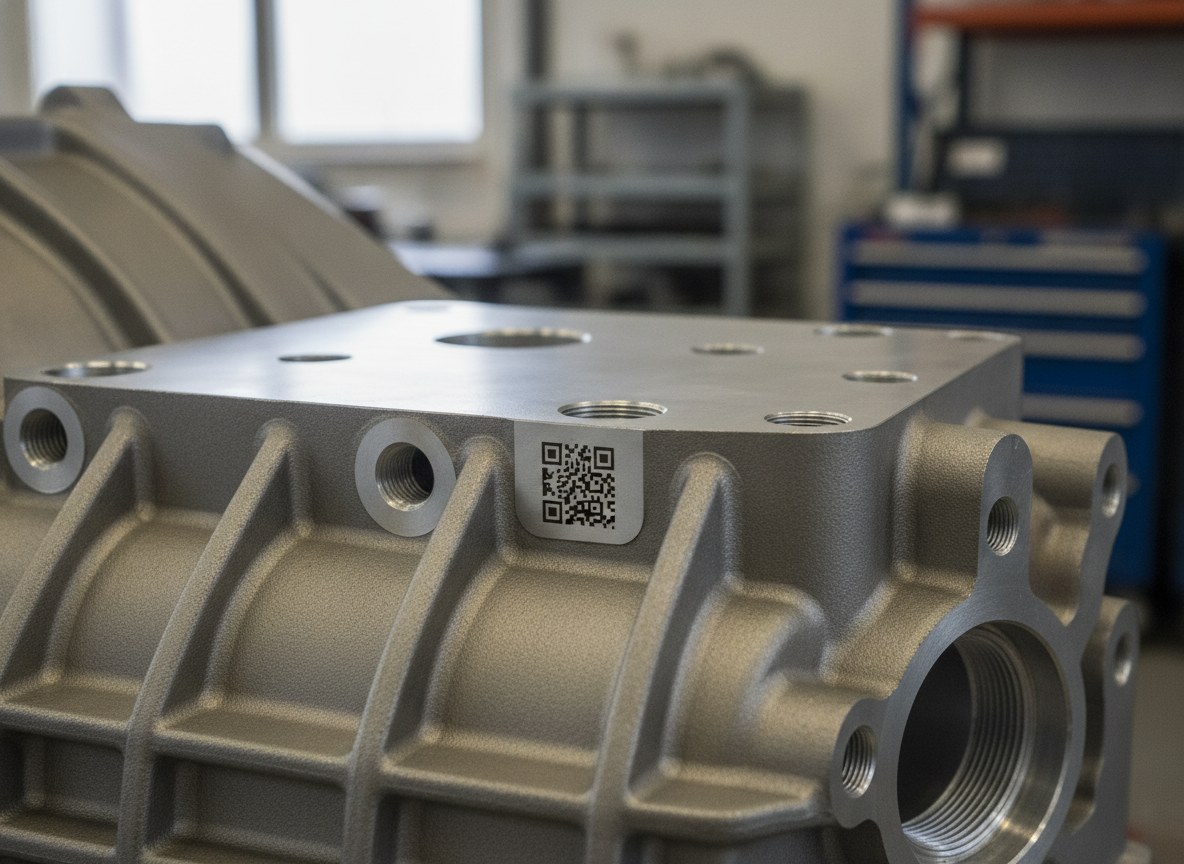
For the data chain, this means the physical carrier of the information is not a weak point. The engraved or annealed code stays, and so does the DataMatrix, which for a given surface holds far more characters than an alphanumeric code and builds in the redundancy needed to be read even when partially damaged. We have already explored this in traceability with DataMatrix on brake discs; here the focus shifts upstream and downstream of the marking, that is, to the data.
Generating and reserving the sequence number
The chain begins before the laser fires. The content of the code — serial, sequence number, structured DataMatrix — is generated or requested from the MES and reserved for the part before marking. Reserving it is not an accounting detail: it is what guarantees uniqueness even when a cycle is interrupted. If a part enters the station, is assigned its sequence number and the cycle then aborts, that number is deemed committed and is not assigned to another part.
The principle that holds up in an audit is that uniqueness and the non-reuse of sequence numbers are governed at system level, not at the level of the individual machine. It is the MES that owns the counter and the assignment logic; the laser marker queries it, reserves, marks and returns the outcome. This way two stations cannot generate the same identifier, and restarting the machine neither resets nor duplicates the numbering.
Data chain in lineReserve serialLaser markingIn-line gradingMatch checkConfirm or quarantinePost-marking confirmation: reading, grading and match
Once the part is marked, the system reads it back. This read-back is the heart of demonstrability: without re-reading, the fact that marking took place remains an assumption. The reading does two distinct things. It verifies the match, that is, that the code read coincides with the one reserved for that part, and it assesses the quality of the code with in-line grading, typically to ISO/IEC 15415 for 2D codes and the AIM-DPM methodology for direct part marking.
Here a distinction that makes the difference in an audit must be held firm: in-line grading is not verification. Grading is a process control that can be applied on the line, cycle after cycle, assigning a quality grade and stopping codes below the threshold. Verification, by contrast, requires a verifier under controlled laboratory conditions — normalised lighting, optics and distance — and serves to certify the conformity of the method, not to validate every single part. Confusing the two, or demanding of an in-line control what belongs to the laboratory, is an error that surfaces immediately in front of the auditor.
| Aspect | In-line grading | Laboratory verification |
|---|---|---|
| Where it happens | On the line, at every cycle | In the laboratory, on a sample |
| Conditions | Production environment | Normalised lighting and optics |
| Purpose | Continuous process control | Certification of the method |
| Outcome | Quality grade of the code | Documented conformity |
No-read, no-match and managing the rejected part
A serious system is judged by how it handles the exception, not the ideal case. If the re-reading fails (no-read) or the code does not correspond to the expected one (no-match), the part cannot continue as conforming. The correct logic isolates the component that has been marked but not confirmed, directs it to controlled handling — traced re-marking or quarantine — and does not let it quietly re-enter the good flow.
Then there is the case of the part that is properly marked and confirmed but rejected further downstream for a defect. Here too the rule is clear: that sequence number belongs to that part and its history, defect included, and is not reused on another component. Recycling a serial to “avoid wasting numbers” is one of the shortcuts that break uniqueness and that a traceability audit spots by cross-checking the records.
Logs and the interface with the MES
Every event in the chain leaves a trace: sequence number reserved, content marked, reading outcome, grading grade, timestamp, station. This log is the documentary proof that, in an audit, replaces the word “I believe” with “the record shows”. For it to be usable it must be aligned with the factory system, not locked inside the machine: the marker communicates with the MES through standard industrial protocols such as Ethernet/IP, OPC-UA and Profibus, becoming an intelligent node of the production line rather than an island.
This is the level where 100% traceability is closed: the physical part and the digital record coincide, uniqueness is enforced by the central counter and every confirmation returns to the system in real time. Our MES and ERP integration software works on this integration between marking and information system, managing the data request, the confirmation and the recording without manual steps.
The errors that lose points in an audit
The weak links recur from one plant to the next. The most frequent ones are few and recognisable:
- marking without re-reading, taking every marking for granted as successful and then being unable to prove the operation took place;
- generating the sequence number without reserving it, with the risk of duplicates on interrupted cycles;
- letting a part that has been marked but not confirmed re-enter the line after a no-read or a no-match;
- reusing the sequence number of a rejected part, breaking system-level uniqueness;
- confusing in-line grading with laboratory verification, or entrusting one with the task of the other;
- keeping the marking log out of alignment with the MES, so that the data in the machine and the data in the factory do not coincide.
It is worth being honest about when all this really matters. A complete data chain — reservation, confirmation, exception handling, log to the MES — is indispensable where traceability has to be audit-proof and the components are safety-critical. On production not subject to IATF 16949, non-safety-critical batches or purely cosmetic marking, a lighter flow can suffice, and over-engineering the architecture adds no value. The point is not to mark more: it is to make the part, the code and the record match — and to be able to prove it.
Software Engineer | LASIT
Software Engineer at LASIT since 2020, Felice Santoriello specializes in the design and development of custom software solutions for customers. He develops tailor-made solutions to integrate and optimize laser marking systems in industrial production processes.


