

Anyone who produces chrome- or nickel-plated brass tapware knows the awkward position marking occupies: it is the last operation in the cycle, it lands on an already finished and polished part, and it is precisely what the customer sees first. It has to carry the brand, the batch references and, increasingly often, a traceability DataMatrix, all without spoiling the mirror finish. But there is a less obvious and more insidious problem: on tapware, marking is also a potential trigger for corrosion.
The electroplated coating is not merely an aesthetic finish: it is the barrier that protects the underlying brass. Every time the beam touches that surface, the quality engineer’s question is not just “does it read well?”, but “am I opening a discontinuity in the deposit that in a few months will become a pitting site?”. Marking chrome-plated brass without compromising the plating is, first and foremost, a matter of controlling energy and choosing the right moment in the production cycle.
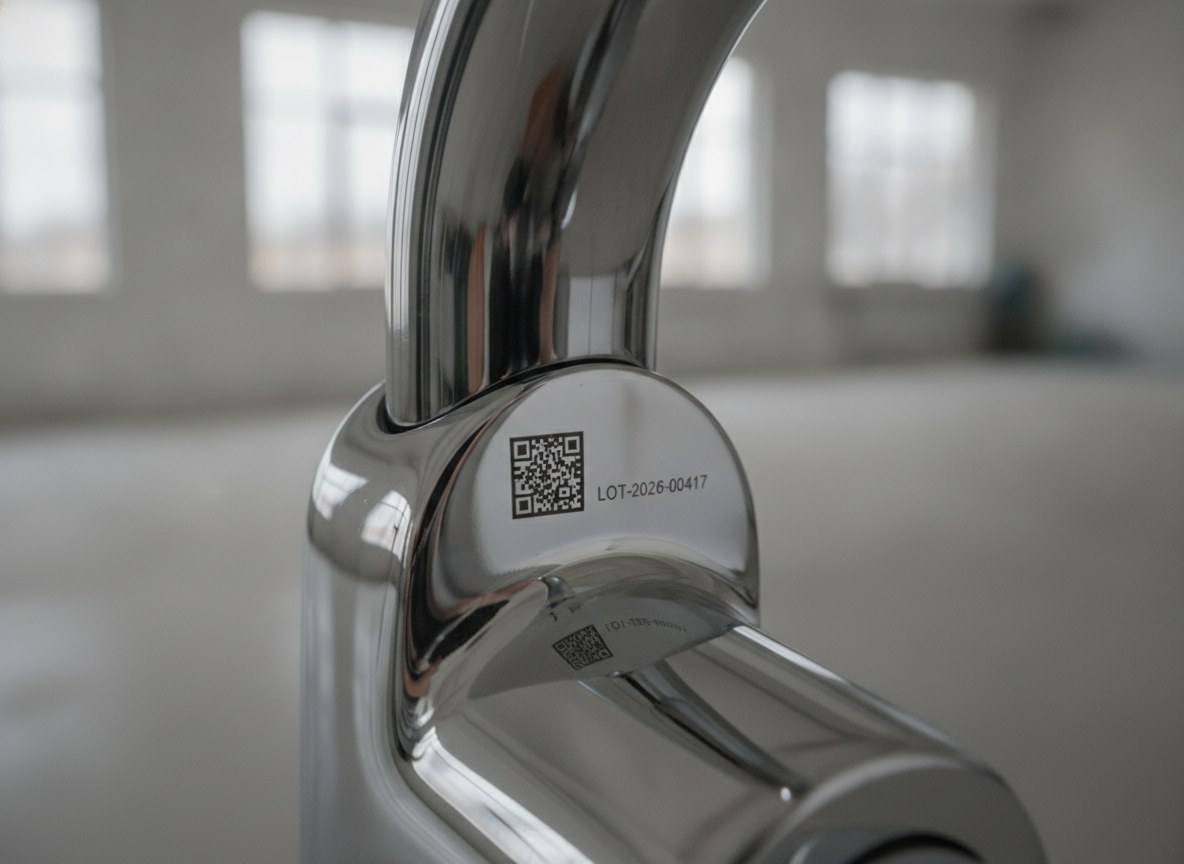
A correct marking on these parts comes from three combined decisions: when to mark relative to the plating, how much energy to work with, and how to demonstrate — before industrialising — that the coating holds.
The coating structure and why marking can trigger corrosion
A chrome-plated tapware part is a stack of layers: the brass substrate, one or more nickel deposits and, on top, a decorative chromium film. The nickel does the heavy lifting of protection and levelling; the chromium, extremely hard and very thin, provides the finish, the scratch resistance and the colour. It is a barrier system: as long as the layers remain continuous, the brass never sees the external environment.
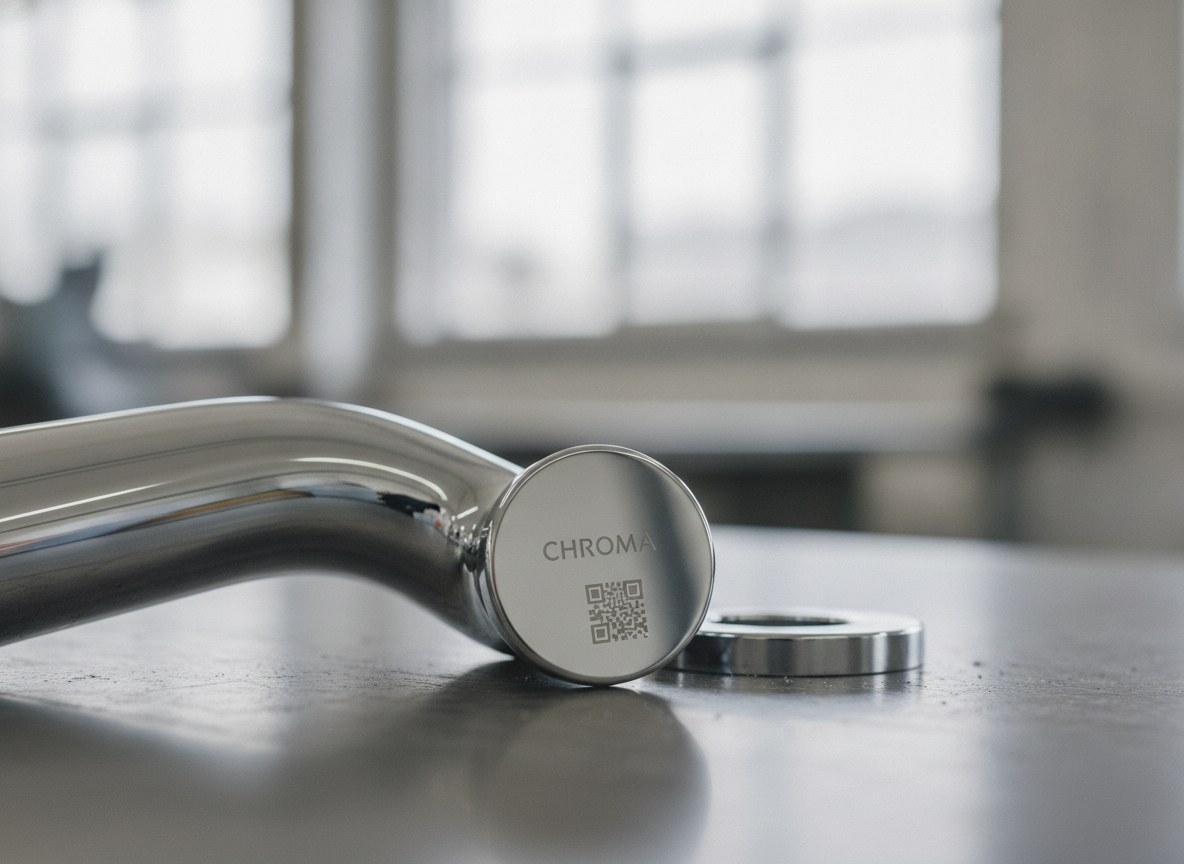
Marking conflicts with this logic when it removes material. If the beam ablates the chromium and cuts into the nickel down to the exposed brass, it creates a discontinuity in the deposit: at that point the coating no longer protects, and in the presence of moisture and chlorides localised corrosion sets in. Making matters worse is the galvanic coupling between dissimilar metals — nickel, chromium and brass exposed together inside a micro-crater — which accelerates the phenomenon. An overly aggressive marking is not merely inelegant: it is a functional defect that surfaces weeks after shipment.
Marking before or after plating: two routes, two trade-offs
The first route is to mark the blank, before plating, and let the electroplated deposits cover the mark. The advantage is clear on the corrosion front: the marking stays sealed beneath the coating, which remains continuous across the entire visible surface. The price you pay is flexibility and sharpness: the levelling typical of the plating bath tends to soften the edges, and on a DataMatrix this means less defined cells; moreover, every part has to be marked upstream, before batch and final destination are known.
| Aspect | Marking before plating | Marking after plating |
|---|---|---|
| Coating integrity | Mark sealed beneath the deposit, continuous barrier | To be checked: possible discontinuity in the deposit |
| Flexibility and serialisation | Tied to the blank, upstream in the cycle | Allows serials and batches applied at the end of the line |
| Code sharpness | Edges softened by plating levelling | Crisp edges and well-defined cells |
| Corrosion risk | Low: no breach on the finished surface | Concentrated here: requires a low-energy process |
The second route is to mark downstream, on the already chrome-plated part. Here you gain everything you lose with the other: serial numbers and batch references applied at the end of the line, crisp edges, high-readability codes. In exchange, this is precisely where the risk concentrates: the beam acts directly on the protective barrier and must be kept under control so it does not punch through. It is the route most used in modern tapware, because late serialisation is often indispensable, but it demands a carefully calibrated process.
When marking is downstream and functional, code quality must be monitored with the same rigour as coating integrity. On the line, two-dimensional codes are graded according to the reference standards, while true verification belongs to controlled laboratory conditions: these are two distinct levels, as explained in the article dedicated to the difference between reading, grading and verifying codes.
Deposit thickness and the laser’s working margin
The critical point is that decorative chromium is an extremely thin layer, on the order of fractions of a micron, laid over a considerably thicker nickel deposit. The margin within which the laser must work, when marking downstream, is therefore narrow: just a few overly energetic pulses are enough to break through the chromium, cut into the nickel and approach the brass. There is no single value valid for all parts, because the thickness of the deposits changes with the plating supplier and the geometry; this is why the correct parameter is found on the real sample, not on a datasheet.
Pulse energy Coating integrity low energy keeps the barrier intactThe logic is that of a threshold: below a certain energy level you obtain contrast through surface alteration, without removing the coating; above it, you begin to ablate material and the barrier thins until it fails. All the fine-tuning consists of staying reliably below that threshold, with a safety margin that accounts for the tolerances of the plating bath.
Detachment and pitting: when there is too much energy
Excess energy does not just remove the coating. Localised heat input can generate micro-cracks in the chromium, which is hard but brittle, and encourage detachment of the deposit at the edges of the mark, in the form of lifting or flaking that widens over time. From there corrosion finds its preferential path: first pitting in the exposed micro-craters, then progression beneath the adjacent coating, where the brass reacts and pushes against the film above.
It is a particularly deceptive defect because at inspection the part looks perfect: the marking is readable, the surface is polished, no one sees anything. The problem only emerges after exposure to the humid environment of a bathroom, and it is the reason why assessing a marking on tapware cannot stop at its immediate appearance.
Low-energy solutions: clear contrast on a polished background
The technical answer is to work in a low-energy regime, with short high-frequency pulses that spread the action across many light micro-interactions instead of a single deep ablation. On these coatings the MOPA fibre source offers the fine control required, as do picosecond regimes, where the thermal impact on the coating is negligible. The aim is not to engrave: it is to modify the surface microstructure in a controlled way to create contrast without opening the barrier. Anyone working with tapware will find further detail on the subject in MOPA technology in tapware.
There is also an aesthetic advantage consistent with this choice. On mirror chrome, a light, satin mark obtained by micro-texturing the surface stands out better than an attempt at a dark mark, which against the reflection would tend to disappear depending on the viewing angle. Light marking on a polished background is at once the most readable and the least invasive, because it stays confined to the outermost layers of the coating.
Verifying integrity with salt spray before industrialising
No parameter should go into production just because it “looks fine”. The integrity of the marked coating is demonstrated with accelerated corrosion tests on samples marked with the same production parameters. The neutral salt spray test according to ISO 9227 is the general reference, but for decorative chromium-nickel coatings the most severe and pertinent test is the CASS (copper-accelerated acetic acid salt spray, ASTM B368), designed precisely to evaluate the protection of these deposits.
In practice, representative coupons and parts are prepared, marked with the candidate cycle, exposed to the test and the marked area is assessed: presence of pitting, coating lifting, corrosion migration from the edges of the mark. Only a cycle that passes this verification on the samples can be considered ready for industrialisation. It is the moment when laboratory fine-tuning stops being an opinion and becomes a repeatable figure, to be locked as a production parameter.
Who it is designed for (and who it is not)
This approach is designed for anyone marking tapware and chrome- or nickel-plated brass components downstream of plating, who has to guarantee contrast and readability on polished surfaces and, at the same time, cannot afford the marking becoming a corrosion site. It is the typical situation of anyone applying a brand, serials and traceability codes to parts destined to last for years in a humid environment.
It is not, however, the obligatory route for anyone with full freedom to mark the blank before plating and no need for late serialisation: in that case, marking upstream and sealing the mark beneath the deposit remains the simplest option on the corrosion front. And it is not needed where the coating has no critical protective function. In all other cases, the practical rule is a single one: define the low-energy parameter on the real sample and validate it with salt spray before opening production.

Applications Manager | LASIT
Applications Manager at LASIT for over 20 years, Mario Palmieri oversees the management and development of the company’s laser laboratory. He is responsible for conducting sample tests for customers, supporting the automotive, medical, aerospace and electronics sectors in identifying the most suitable laser marking solution for their needs.


