
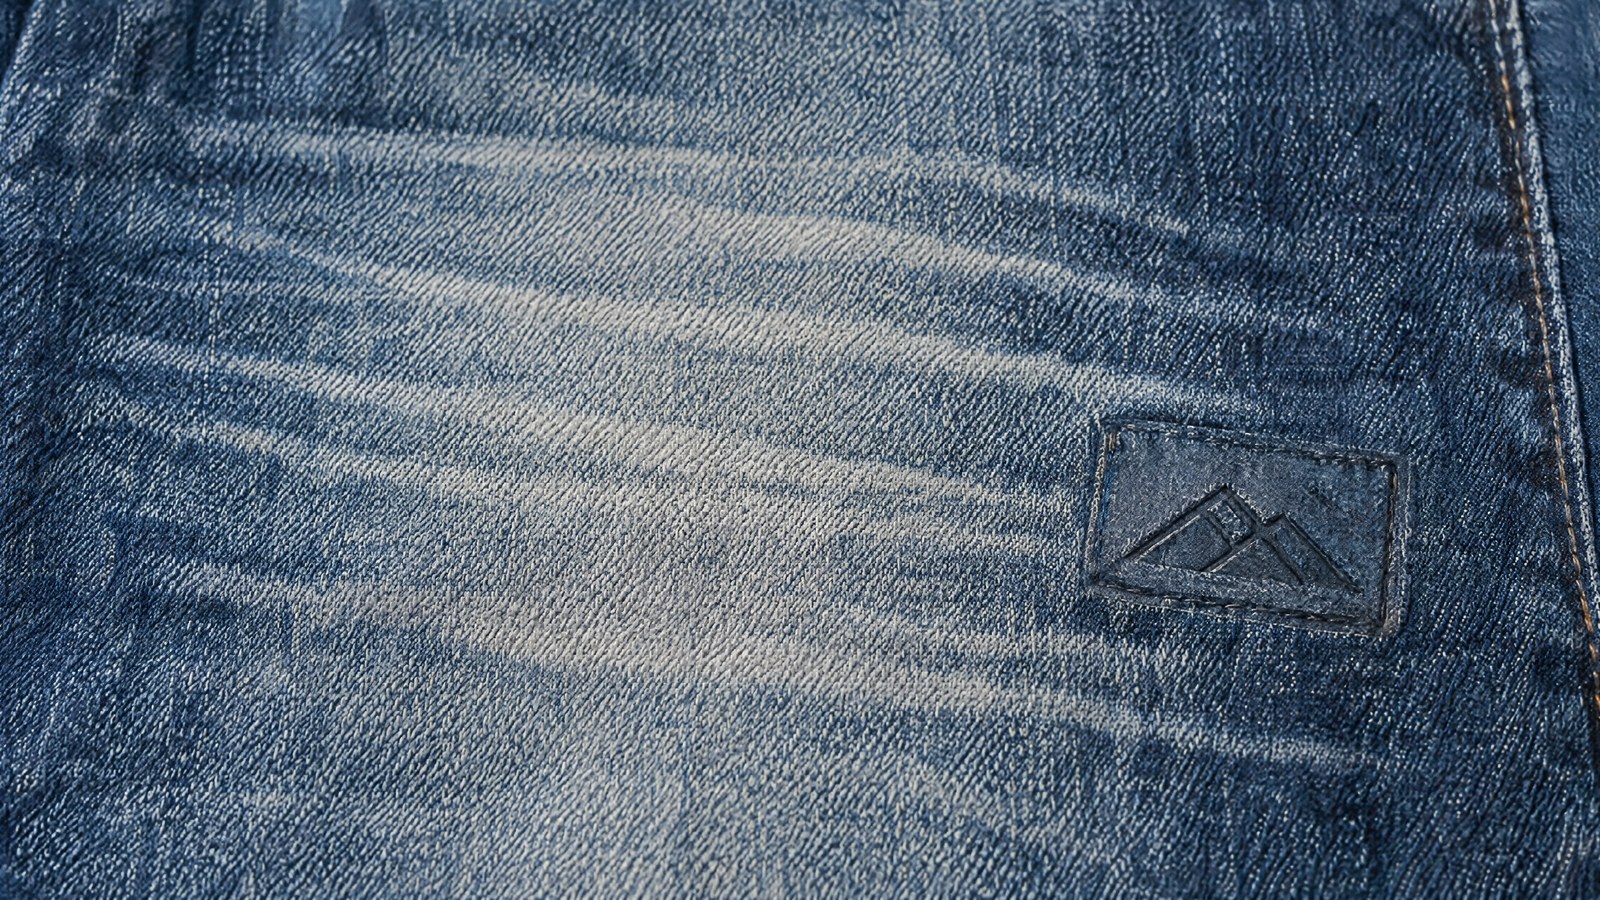
Anyone running finishing operations in textiles and leather goods knows how much the washing department weighs on the process: denim bleaching relies on permanganate, hypochlorite and pumice baths, on manual sandblasting and on rinse cycles that consume water and generate effluent to be treated. On leather, local design and colour often come from mordanting, hot stamping and chemical treatments. These processes are effective, but variable, slow to retool and costly in environmental terms.
The laser steps in precisely at this point. It is not the alternative to a print applied onto the fabric: it is the alternative to the chemical-water process that lightens, engraves and shapes the material. The beam acts directly on the surface — it degrades the dye, ablates the outermost layer, cuts the profile — using optical energy in place of water and reagents.
For a production or quality manager this means three things at once: a result that repeats identically batch after batch, a cycle that is retooled by changing a file instead of a bath, and a dry process that eliminates effluent and offcuts. It is worth seeing where it genuinely works — and where it does not.
The laser replaces the chemical bath, not the print
The distinction matters. A print deposits pigment on top of the fabric; the laser adds nothing, it modifies the material that is already there. On denim it removes the surface dye, revealing the lighter cotton beneath; on leather it ablates a thin layer of finish or grain; on acetate it melts and separates the edge along a clean profile. It is the same principle, applied with different energies: unlike when you replace inkjet printing, here no mark is laid down but the surface is transformed.
| Process aspect | Chemical-water process | Laser process |
|---|---|---|
| Water consumption | High, across baths and rinses | None |
| Chemical agents | Oxidisers and mordants | No reagents |
| Material offcuts | Dedicated dies and cut-outs | File-driven layout, optimised cutting |
| Tone repeatability | Tied to concentration and bath time | Defined by digital parameters |
| Residue management | Liquid effluent to be treated | Air extraction and filtration |
The most immediate practical benefit is that the entire design lives in a vector file. Changing the effect, position or intensity does not require redoing a bath or a die: you edit the path and relaunch the cycle, with recorded and reproducible parameters.
Denim bleaching without water or oxidisers
Denim owes its colour to indigo, a dye that fixes onto the outer part of the cotton fibre while leaving its core light. It is precisely this structure that makes it ideal for the laser: a CO₂ source at 10.6 µm, well absorbed by natural fibres, degrades the indigo on the surface and brings out the lighter tone beneath, without affecting the weave.
By adjusting the beam energy you obtain graduated lightening: from whiskers and localised abrasions through to extended designs and patterns, all in a single dry pass. The degree of lightening is a direct function of the energy deposited, and is therefore continuously controllable.
Beam energy Lightening degree The tone is set by the parameters, not the bath.Compared with the traditional cycle, permanganate, hypochlorite and pumice disappear, and with them the baths and rinses: it is a water-free finishing, in line with the process sustainability goals the fashion sector is setting itself.
Engraving on leather and split leather: a controlled mark
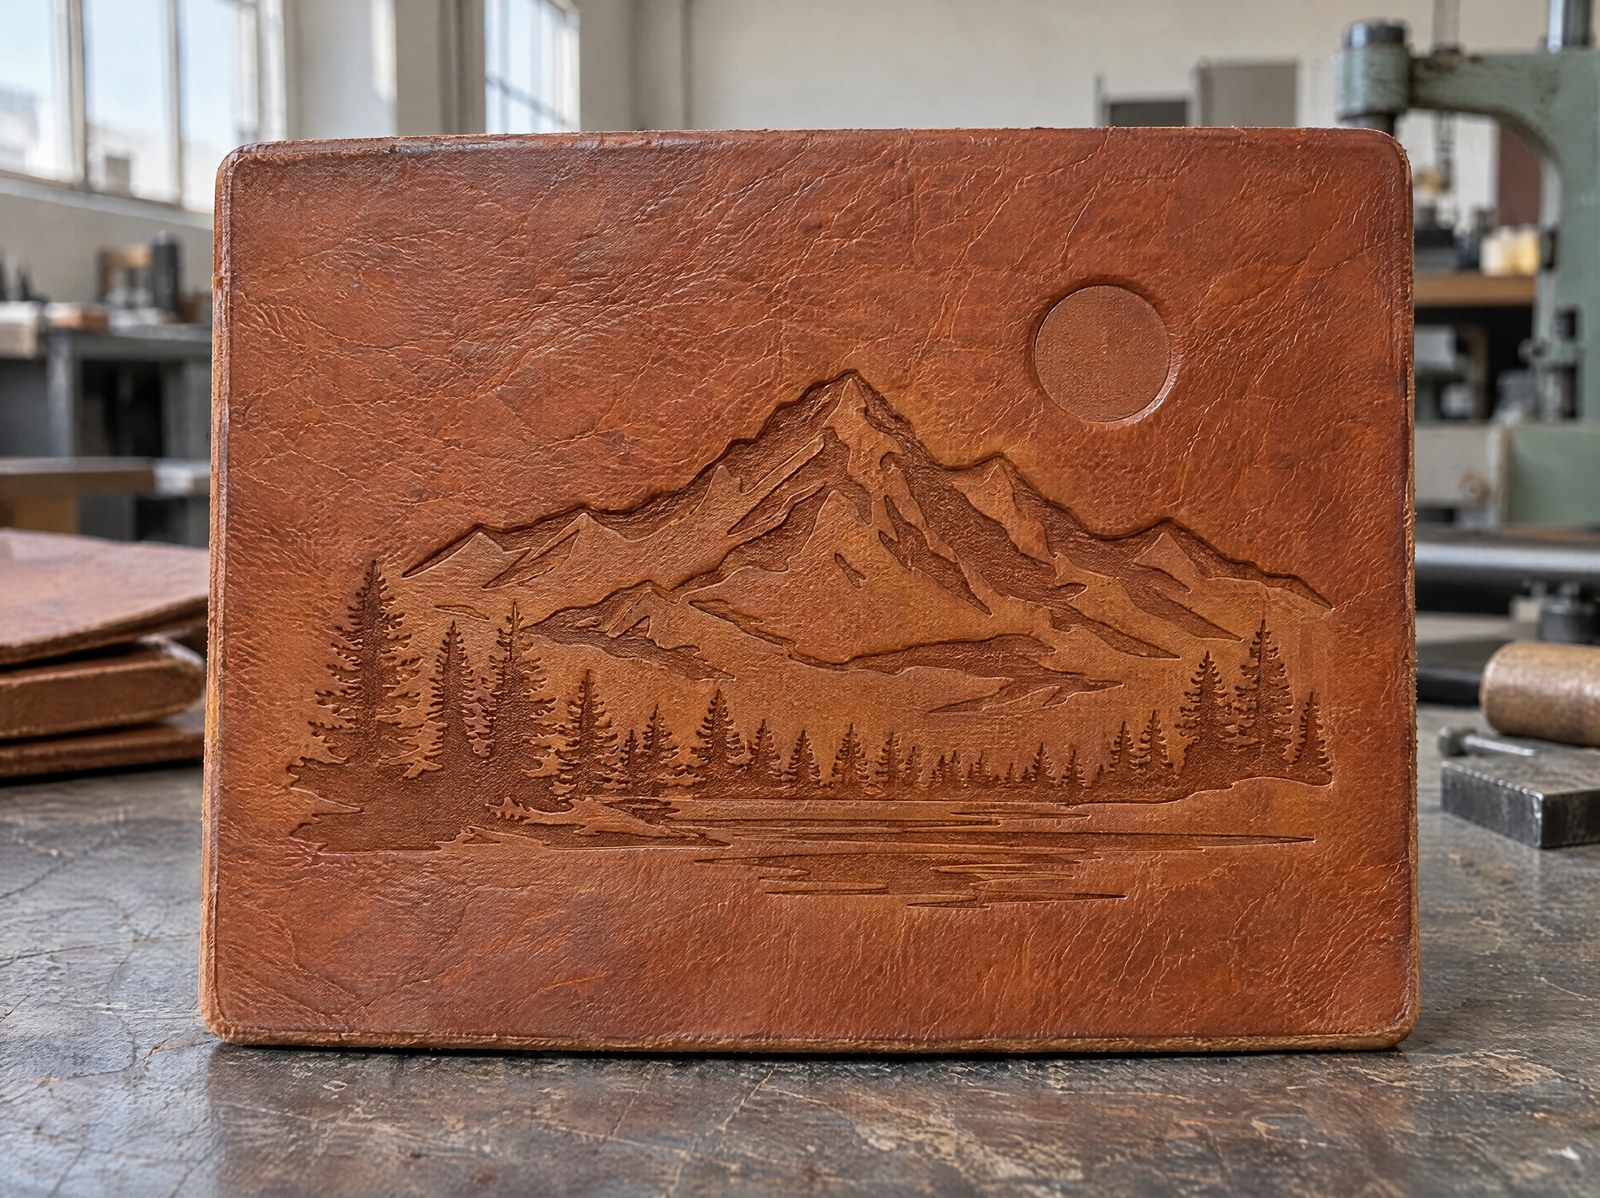
On leather the laser works by ablation: it selectively removes the outermost layer and generates a contrast that depends on the material and the parameters, not on an ink. On full-grain leather, on split leather and on finished hides you obtain logos, monograms, textures and decorations with consistent depth and sharpness.
The result requires neither mordanting nor hot stamping with dedicated clichés. The design is digital, and therefore customisable piece by piece — useful for capsules, numbering and personalisation — while keeping the same mark across the whole series.
Cutting, perforation and working acetate
The same beam that lightens and engraves can cut and perforate. On technical fabrics and synthetics, laser cutting produces a clean edge and, on thermoplastic materials, a sealed one that limits fraying without additional finishing. Perforation patterns, often impractical with a mechanical die, become simple vector paths.
Cellulose acetate, widespread in accessories and eyewear, lends itself well to controlled cutting and engraving: the beam works the profile and the details with clean edges. Because the layout is digital, changing model means loading another file, with no need to tool up new dies and with a nesting that reduces material offcuts.
Fumes, odours and dedicated extraction
Dry-working organic materials such as cotton, leather and acetate generates fumes and odours: this is the point that calls for the most attention in a laser finishing system. It is not a detail to be overlooked, but a design requirement. Stable processing requires extraction systems and filtration sized to the material and the production volume, which capture residues at the point of processing and keep the optics clean.
The advantage is that here we are talking about air management, not liquid effluent: residues are captured and filtered locally. This is an aspect that deserves a dedicated look at extraction systems in laser marking machines, because both the quality of the result and the conditions in the department depend on it.
Tone repeatability, batch after batch
The historic limitation of wet processes is variability: the outcome of a bath depends on concentration, temperature and immersion time, and two batches treated some time apart are rarely identical. The laser reverses this logic. Tone, depth and design are defined by numerical parameters saved in the processing programme, and are therefore independent of the operator and of the ageing of a bath.
Across broad product families this translates into aesthetic consistency between garments, between sizes and between reorders months apart — an aspect that, in fashion, weighs as much as the quality of the individual piece. Visual inspection remains part of the cycle, but it starts from a stable, documented baseline.
Who it is intended for (and who it is not)
Laser finishing is at its best where the material is homogeneous and predictable: denim, finished and coated hides, technical synthetics, acetate. In these cases the tone is controlled and repeatable, the cycle is dry and the model change is immediate.
It should instead be approached with caution on very natural and non-uniform hides — vegetable-tanned leathers, aniline full-grain with veining and variable absorption: here the same energy can give different tones from one area to another, and colour consistency is not guaranteed. On these materials the laser remains useful for engraving and decoration, but the promise of uniform tone should be verified beforehand on real samples.
In short: if your finishing today depends on chemical baths, water and sandblasting, and you need a repeatable, dry result on denim, finished leather or acetate, the laser tackles exactly those steps. If you work with natural, living hides, it should be tested in the field before industrialising it — and that is precisely what a test on samples allows you to establish.

Public Relations Manager | LASIT
Public Relations Manager at LASIT since 2019, Claudia Neri is responsible for managing the Marketing and Communications department. She handles the company’s communication strategy, coordinating public relations, brand promotion and institutional communication activities for the Italian and international market.


